Façade cassettespro
Carved star cassette
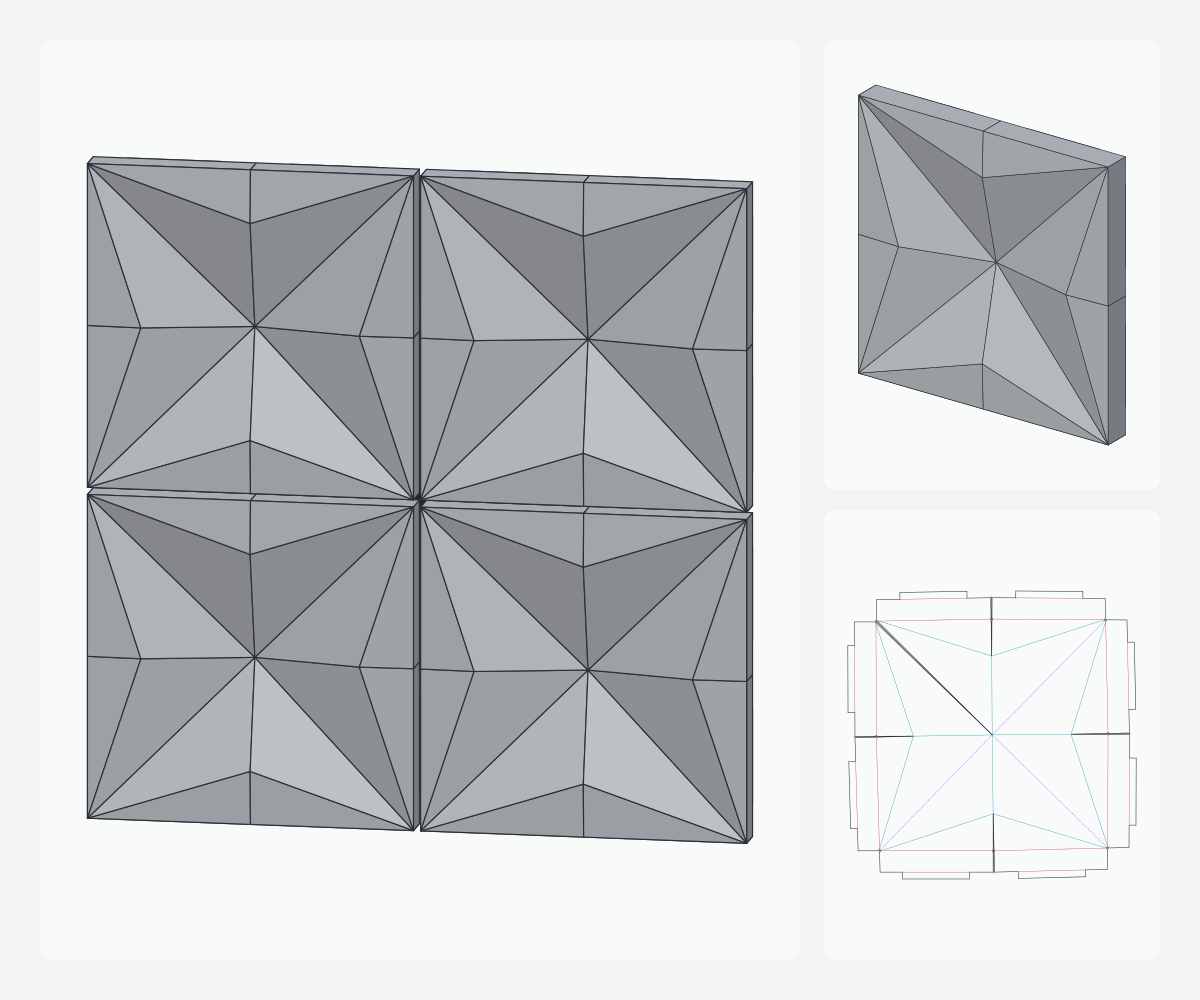
The four-point star carved INTO the panel: the centre sinks to the bottom of a hollow, four valleys dive into it from the corners, and four points rise at the middle of the sides. Plain rectangular outline, sixteen facets, grooves on the visible face.
Open in the studio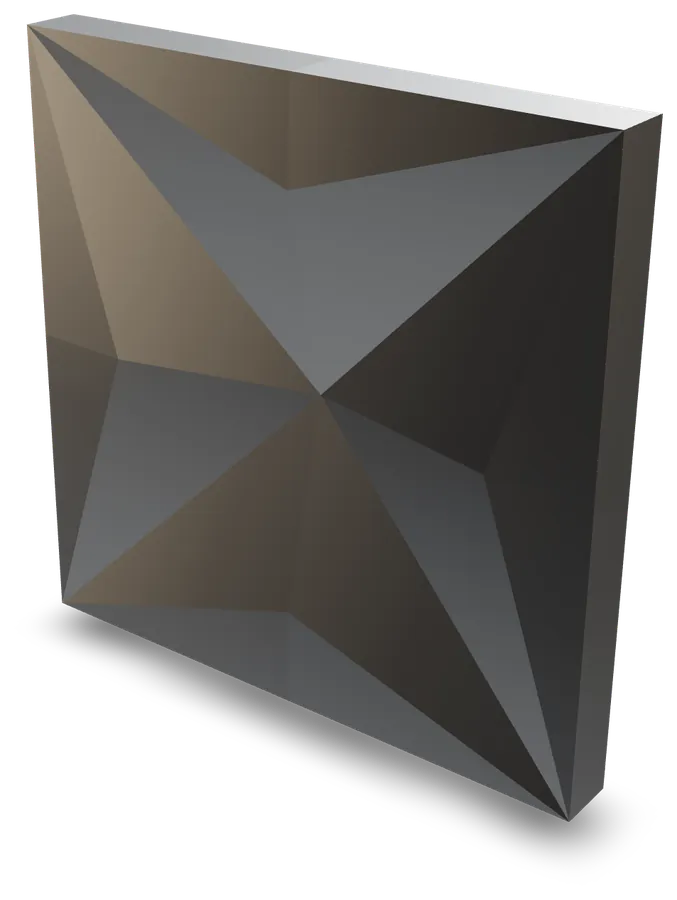
ACM 3D Studio
- Developed
- 756.4 × 755.5 mm
- Material
- ACM 4 mm
- Folds
- 31
- Mark
- star-hollow
Fabrication data
Carved star cassette — at 600 × 600 mm in 4 mm ACM, this family unfolds into a 756.4 × 755.5 mm flat pattern with 31 folds, including 1,280 mm of groove machined from the visible face, with the sheet flipped for that pass. A 1,500 × 3,200 mm sheet holds 4 of them, for 56.5 % waste.
- Material per panel
- 0.522 m²
- Folds
- 31
- Total groove length
- 8,445 mm
- Cutting length
- 6,304 mm
- Corner slits
- 9
- Corner reliefs
- 8
V-grooves (apex angle)
- 16.5°2,528 mm
- 87.9°2,402 mm
- 90°1,408 mm
- 26.4°1,280 mm
- 10.2°827 mm
Panels per sheet
- 1,220 × 2,440 mm3(47.4 % waste)
- 1,500 × 3,200 mm4(56.5 % waste)
DXF layers
- CONTOUR6,304 mm
- RAINURE_903,810 mm
- RAINURE_1603,355 mm
- RAINURE_AVANT_135front face1,280 mm
The names and colours your CAM software will show. RAINURE_AVANT: fold concave on the visible face, sheet flipped for that pass.
Computed by the engine at the default parameters, on 4 mm ACM and the reference router. Your own machine and material profiles change these values in the studio.
Parameters
| Parameters | Range | Default |
|---|---|---|
| Width | 200 – 3,000 mm | 600 mm |
| Height | 200 – 3,000 mm | 600 mm |
| Relief height | 35 – 120 mm | 45 mm |
| Point position | 12 – 38 % | 33 % |
| Point height | 3 – 45 % | 8 % |
| Return depth | 0 – 200 mm | 60 mm |
| Fixing tabs | — | ✓ |
| Tab width | 10 – 60 mm | 20 mm |
PresetsCarved starDeep hollowPronounced points
Manufacturing constraints
- The return must exceed the groove width plus half the bend deduction, or the groove eats into the return.
- Facet-to-facet folds are grooved with the smallest cutter of the profile, V left open: the angle is held by the geometry. The angle between two facets must not exceed that cutter’s apex angle.
- Vertical returns, all tabs flat in the −D plane (rail mounting). The facet-to-return fold is 90° ± slope: below 90°, the 90° cutter is left open and the return is held by the riveted tab; above 90° (facet descending towards the edge), a wider cutter (60° nominal = 120° apex) or the machine profile’s overfold tolerance is needed.
- Every raised vertex requires a V-slit to the edge (a flat sheet has 360°, the relief less). Near the vertex the slit is narrower than the contour tool: it is cut along its axis and the tool bites each facet by up to Ø/2.
- Tabs are shortened at every corner and every kink of the edge so they never collide behind the panel: by (return + 2 mm), and more on a sharp corner, where the bisector must be cleared (tab width ÷ tan(angle/2)). An edge too short gets no tab.
- The bottom of the hollow sinks BEHIND the face of the panel: it must stay at least 5 mm in front of the tab plane, otherwise the relief hits the framing and the cassette no longer sits flat on its rails. A carved star therefore needs a deeper return than a raised cassette.
- A V-groove is cut on the CONCAVE side of the fold. Here the only valleys are the ones diving from the corner into the bottom: they go to the RAINURE_AVANT_* layer, machined visible-face up with the sheet flipped — one of the four is absorbed by the bottom’s slit, so three remain. Everything else, points included, is grooved on the back. That is far fewer cuts into the coating than a raised star, where the rim of the notch is what turns into a valley.
- The central bottom must stay a POINT (pointing backwards): the plane angles of the eight facets meeting there must sum to less than 360°. Raising the points opens it up, and past the limit the bottom becomes a saddle, which flat sheet cannot take. The cure: carve deeper, or move the points towards the edge.
- At 33 %, each point lands on the centroid of the triangle formed by the two corners of its side and the panel centre — the rule of thirds of the reference sheets. Closer to the edge, the point becomes a narrow ridge that takes far more height; closer to the centre, the valleys widen but the bottom flattens fast.